Reorder when the stock you can sell falls to the sales you expect during your lead time, the days from placing an order to the stock arriving, plus a buffer. Picture a bestseller down to its last sizes, with the next drop still weeks away. Order later and the new batch lands after the shelf is empty, and order too early and cash sits in stock that does not move. If you are planning a range, our private label clothing page is a good place to start, and the steps below show when the next order should go in.
The reorder point is the stock level at which you place the next order. The University of Kentucky course notes give it as daily demand multiplied by lead time, plus safety stock. Safety stock is the buffer inside that figure. King’s article on safety stock defines it as inventory carried to prevent stockouts, and stockouts come from fluctuating demand, forecast error and variable lead times.
Here are the sums with example figures, not a forecast. Average daily sales of 4 pieces and a lead time of 36 days give a lead time demand of 4 x 36 = 144 pieces. Add a safety stock of 15 pieces, worked out under the buffer heading below, and the reorder point is 144 + 15 = 159 pieces.
Measure lead time from your own purchase order dates to the day the goods are received, not from the quoted date. A quote is a plan, and your own record is the figure that decides when the shelf runs out.
Table 1 lists each input, where its number comes from and the mistake to avoid.
|
Input
|
Where the number comes from
|
The mistake to avoid
|
|---|---|---|
|
Average daily sales
|
Units sold per day for that style and size, from your POS or sales report over a settled period
|
Using a launch week, when sales run faster than normal
|
|
Lead time in days
|
Your purchase order date to the day the goods are received
|
Using the quoted lead time instead of the one you achieved
|
|
Safety stock
|
The service level you choose, applied to how much your sales and lead time vary
|
Setting it by habit, with no service level behind it
|
|
Sellable stock on hand
|
Units you can sell today, net of wholesale orders already committed
|
Counting damaged, held or committed units as available
|
|
Open orders
|
Purchase orders already placed, with their expected arrival dates
|
Forgetting them, so the same gap gets ordered twice
|
Compare the reorder point with sellable stock plus open orders, so a gap that is already covered by an order is not ordered twice. Treat the table as a checklist for every reorder, not a one-time setup. One guessed input makes the whole answer a guess.
Sell-through rate is units sold divided by units received, multiplied by 100. This is the common retail convention, not a formula from a standards body, so use it to compare your own lines with each other.
Measure it per size and per colour, not across the whole style. A blended figure can look healthy while one size has sold out and another has not moved, and the reorder then goes to the wrong sizes. Net returns out of units sold first, so a unit that came back to the shelf is not counted as a sale.
Leave pre-orders out of the calculation as well. A pre-order sells stock that has not arrived yet, so it says nothing about how the received stock sold, and units still in transit have not reached the shelf to be sold from.
Vendor guides quote sell-through bands, but the sources behind this guide do not give one. Compare each size with its own last season and with the reorder point above, rather than with a published range.
Days of cover tells you how long your sellable stock lasts at your current pace. The Virginia Tech extension publication on days’ sales in inventory describes the ratio as an indication of “the length of time it will take to use up the inventory through sales”. That ratio is calculated from cost, so for units the arithmetic here is a unit version of the same idea: sellable units divided by average units sold per day, with open orders added to the units when they are already on the way.
Example figures again: 120 sellable pieces at 4 sold a day give 120 divided by 4, which is 30 days of cover. Divide 30 by 7 for weeks, which is about 4.3 weeks. That week conversion is this guide’s own arithmetic, not a published formula.
The two tests agree on the answer. The reorder point is 159 pieces and you hold 120, so you reorder now. The cover test says the same, because 30 days is less than the 36-day lead time plus a buffer of 3.75 days (15 pieces divided by 4 a day).
In this example the order is already late. Even an order placed today lands on day 36, six days after the 30 days of cover run out, so plan for about six days without stock or find units to cover that gap.
Work back from the date the stock must land. A repeat built from your own spec has three stages, and on our timings they add up to 36 days: 12 for the sample, 18 for bulk and 6 for shipping.
The MOQ post says that when a design is built from your own spec rather than an existing base, every order still goes through a physical sample before bulk starts. Put that sample into the repeat date you give your team from the start.
The order date is the date the stock must land, minus 36 days. Put that order date in the calendar and move it earlier whenever your own lead time record shows the factory running long. Keep the three stages in view, because a late sample approval moves every date after it.
The buffer is set by two things: how much your sales vary and how much your lead time varies. King calls the share of replenishment cycles that end without a stockout the cycle service level, and gives typical goals of 90 to 98 percent. King notes that higher service levels need disproportionately higher Z values, so each step up needs more buffer than the one before.
Table 2 gives the Z value for six service levels, taken from King’s table. The Z value is how many standard deviations the buffer has to cover, and a standard deviation measures how far your sales swing around their average.
|
Service level
|
Z value
|
Cycles with a stockout (100 minus the service level)
|
|---|---|---|
|
84 percent
|
1.00
|
16 in every 100
|
|
90 percent
|
1.28
|
10 in every 100
|
|
95 percent
|
1.65
|
5 in every 100
|
|
97 percent
|
1.88
|
3 in every 100
|
|
98 percent
|
2.05
|
2 in every 100
|
|
99 percent
|
2.33
|
1 in every 100
|
King notes that a Z value of 1 covers one standard deviation, which gives enough inventory in 84 percent of cycles. For demand variation, King’s formula is safety stock = Z multiplied by the square root of the lead time divided by the period your sales data use, multiplied by the standard deviation of demand. For lead-time variation, it is safety stock = Z multiplied by the standard deviation of lead time, multiplied by average daily demand.
Example figures, not a forecast: daily sales have a standard deviation of 1.5 pieces, the lead time is 36 days, the sales data are daily and the service level is 95 percent. Safety stock = 1.65 x the square root of (36 divided by 1) x 1.5 = 1.65 x 6 x 1.5 = 14.85, which rounds up to 15 pieces.
When demand and lead time both vary, and the two do not depend on each other and are normally distributed, King’s combined formula takes Z multiplied by the square root of the sum of the two squared terms. If they do depend on each other, King says to add the two separate calculations instead. In his worked example, demand variation has almost ten times the effect of lead-time variation, so the sales record is the first place to look. King also warns that setting the buffer at 10 or 20 percent of cycle stock, a common shortcut, generally results in poor performance.
King also suggests setting the Z value for each group of products by its importance to the business, so high-value styles carry more buffer. He adds that fill rate, the share of ordered volume you can actually supply, is often a better measure than cycle service level, because cycle service level counts stockouts without regard to their size.
Order enough to cover the sales you plan for after the batch lands, and keep the safety stock out of that count. In the example, 4 pieces a day for 60 days is 4 x 60 = 240 pieces, and the 15 pieces of safety stock stay on top as the buffer for a late week or a fast one.
The economic order quantity (EOQ) model finds the order size where the yearly holding cost (the cost of keeping stock on the shelf) equals the yearly ordering cost (the cost of placing orders). The University of Kentucky notes list its assumptions: the order arrives instantly, there is no stockout and demand is constant. A factory minimum and a fabric minimum set the smallest order you can place, so treat any EOQ result as a check on the order, not as the order size.
A size curve is the share of the run each size takes. Split the total by each size’s share of recent sales: in the example, 240 pieces at 20 percent for S, 35 percent for M, 30 percent for L and 15 percent for XL gives 48, 84, 72 and 36 pieces. These shares are example figures, so use your own sales by size, and check that the total still clears the minimum order quantity for your design.
How each size is graded from the base pattern is a separate step, covered in what pattern grading is. This section only sets how many pieces of each size you buy.
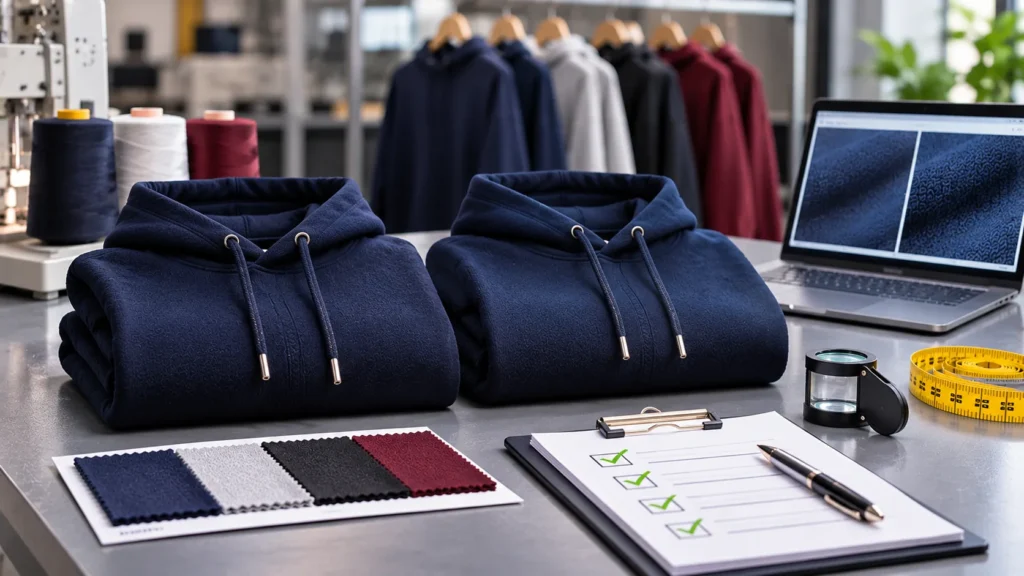
A reorder has to match the approved sample on more than colour. Fabric weight, trims, labels and the size chart all come from the tech pack for the first run, so that tech pack is the reference for the second. Keep the tech pack version and the approved sample with the order number, so the factory can see which spec each reorder follows.
A reorder is a new dye lot, and the fabric dyeing guide explains why it is checked against the original approved standard rather than assumed to match. Keep the original lab dip (the small dyed swatch approved before bulk) on file as that standard, and have the mill document the dye recipe from the first run. Our fabric sourcing page says “We do not use stock dye lots.” For a custom colour, plan the reorder as a new dye run and ask us how long that adds, because the 36 days above do not include it.
The fabric sourcing page says a custom Dye-to-Match (DTM) run “typically requires a minimum of 300 to 500 kilograms of fabric per colorway”, where a colourway is one colour version of the design. Check that quantity before you size a reorder in a custom colour, because it is a fabric figure and not your garment count.
Our MOQ is 30 per design, so check your reorder quantity against that number before you send it. A repeat built from your own spec still goes through a physical sample before bulk starts, and the sample, bulk and shipping stages then take the 36 days set out above.
Our apparel prototyping and sampling page calls the approved pre-production sample the “Golden Sample”, and says quality control inspectors use that garment as the absolute benchmark. Keep it on file with the approved spec and the order number, so each reorder can be checked against the same garment.
Table 3 sets out each reorder trigger, what to check first and what to send us.
|
Reorder trigger
|
What to check first
|
What to send us
|
|---|---|---|
|
Sellable stock reaches the reorder point
|
Sellable units net of committed orders, plus open orders, and the days of cover
|
Your stock count by size and colour, and the quantity you want
|
|
The style, fabric or a trim has changed
|
The tech pack and bill of materials against the approved sample
|
The updated tech pack and the approved Golden Sample
|
|
The colour is custom
|
Whether a new dye run is needed, and the fabric quantity for that colourway
|
The colour reference, such as a Pantone code or a physical swatch, and the approved lab dip
|
|
The size split has changed
|
Your share of sales by size from the last settled period
|
Your size split and the size chart you sell with
|
|
The arrival date is fixed
|
The work back from that date: 12 days of sample, 18 days of bulk and 6 days of shipping
|
The arrival date you need and the date you want the sample approved by
|
Send these items through our contact page, and use the upload field for PDF, PNG or JPG files. A full refund or a free remake is what you get if the order does not match what was agreed.
There is no fixed interval. A reorder goes in when sellable stock reaches the reorder point, so a fast seller can need an order much sooner than a slow one. Check the count often enough that every check still leaves time for the lead time to run.
The sources behind this guide do not set a sell-through rate for a reorder. The common retail convention is units sold divided by units received, multiplied by 100, and you should compare that figure with your own last season and with the reorder point. Use it as one input beside days of cover, not as a pass mark.
No. According to King's example, a 95 percent service level still expects a stockout in about 5 in every 100 replenishment cycles. A higher service level cuts that share, but it needs a larger buffer, so choose the level your customers and cash can carry.
There is no universal number, because the buffer depends on the service level you pick and on how much your sales and lead time vary. Set the service level first, then calculate the buffer from your own sales record, as the worked example in this guide does. A rule of thumb skips that step, so do not use one as a substitute.
Plan for a sample on any repeat built from your own spec. Our MOQ page says that when a design is built from your own spec rather than an existing base, every order still goes through a physical sample before bulk starts. Put the sampling days into the date you give us, and send the approved spec with the order.
Yes. Net returned units out of units sold before you read the sell-through rate, so a sale that came back is not counted as demand. Returned units that are clean and sellable again count as stock on hand, and damaged returns do not.
Count only sellable units that are not already promised to a buyer. A committed wholesale order comes out of stock on hand, so a count taken before those orders are picked can make the reorder point look safe when it is not.
Stop when the sellable stock you hold would last longer than the selling time left in the season, because each extra unit then has to be cleared at a markdown. Compare days of cover with the days left to sell before every reorder.
Use the lead time you achieved. Measure it from the purchase order date to the day the goods are received, and update the figure after each order, because a quote is a plan and your record shows what the factory delivered.
FOUNDER & CEO AT RIJIZ