In the apparel industry, Cut, Make, and Trim (CMT) is the ultimate test of a factory’s mechanical discipline. When you choose a CMT production model, you are acting as the primary supplier. You have spent months sourcing the perfect raw denim, the ideal custom-dyed French Terry, or a highly technical activewear blend. You are shipping thousands of dollars of your own raw material directly to our loading dock.
If a blade shifts by a millimeter on the cutting table, or if a sewing operator applies too much tension to a four-way stretch fabric, your proprietary textile investment is destroyed.
We provide CMT manufacturing services built on strict industrial accountability. We do not use hand-scissors for bulk runs, and we do not hide our fabric consumption data. We deploy automated laser-guided CNC cutters, specialized industrial sewing machinery, and transparent yield reporting to ensure your approved Golden Sample is replicated flawlessly across thousands of units.
Amateur brands obsess over the sewing phase, but the cutting room is where the profit margins of a CMT run are won or lost. How your raw fabric is laid out, tensioned, and sliced dictates your raw material waste and the final drape of the garment.
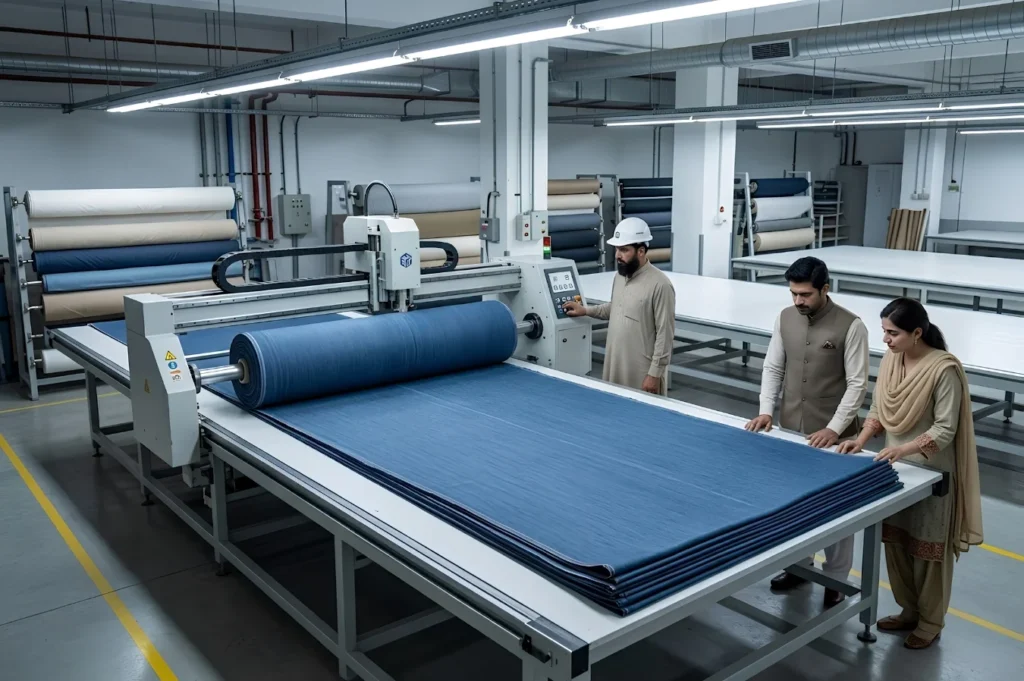
Before any blade touches the cloth, the rolls you send us are unwound and stacked onto cutting tables in layers called "plies." If the cloth is drawn taut while it is spread, it locks in kinetic tension. When the pieces are cut, that stored tension lets go and the panels shrink right away. A cutting room without automated, zero-tension spreaders will return garments that measure smaller than your approved pattern.
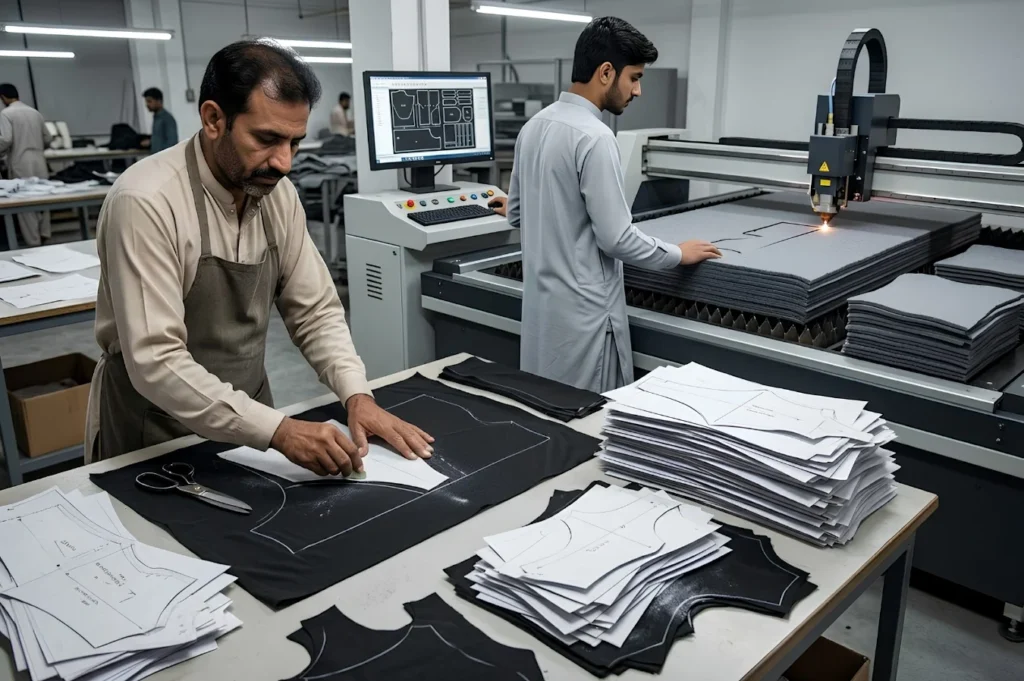
Hand tracing and shear cutting work for a lone prototype, but they are disastrous for bulk runs. Our floor runs automated CNC (Computer Numerical Control) cutters. Your DXF marker files go straight into the cutter, which slices heavy 450 GSM fleece or delicate activewear to micro-millimeter precision.
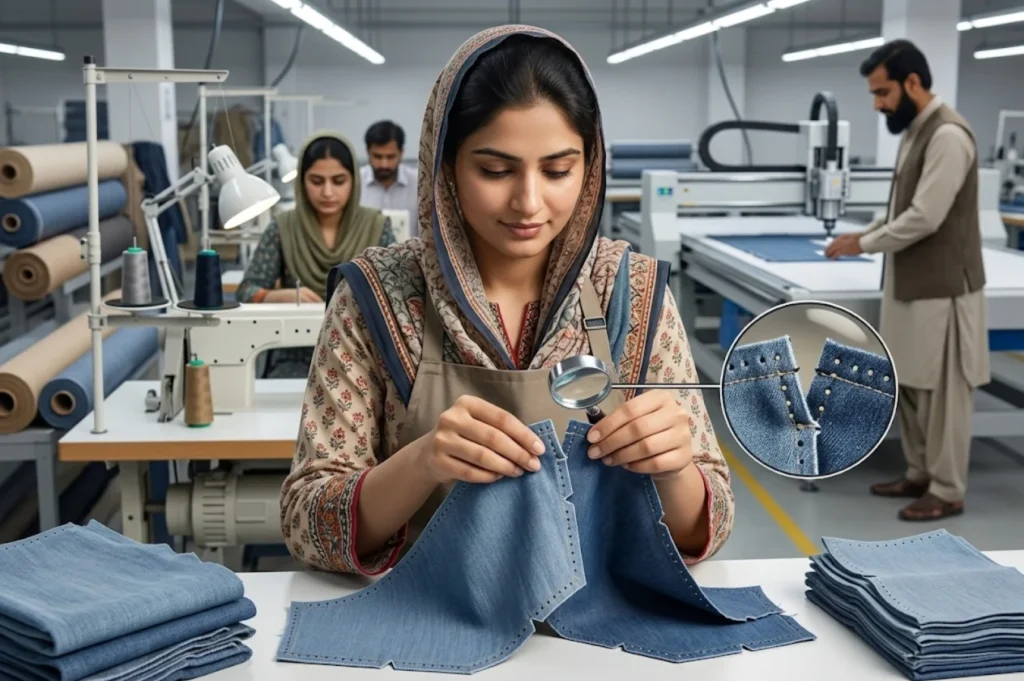
A sewing operator should never have to guess where a pocket goes or how a sleeve aligns with a shoulder. During the CNC cutting phase, automated drills punch microscopic holes and cut V-notches into the perimeter of the fabric. These industrial markers lock the pieces together perfectly, completely removing guesswork from the assembly line.
A basic straight-stitch machine is not enough for a complex technical garment. Each fabric and each load-bearing seam calls for its own machine setup, thread, and stitch type. A premium CMT apparel production facility must maintain a diverse fleet of specialized machinery to prevent seam failure.
Stitch four-way stretch spandex on a rigid lockstitch and the thread breaks the first time someone pulls it on. Our athletic and performance runs use 4-thread overlock and coverstitch heads. Their looping thread moves with the cloth, so the seam flexes as the fabric does. We also apply flatlock stitching, which keeps inside seams from rubbing on snug athletic fits.
Sewing 14oz raw denim or heavy canvas demands serious mechanical torque. Ordinary machines skip stitches or snap needles when attempting to push through several layers of heavy cloth. Our heavy-duty walking-foot machines pull the thick plies through the needle plate evenly, so the top layer stays flat and does not shift out of alignment.
Workwear and premium streetwear have to survive hard, repeated stress. Our bar-tack heads are programmed to lay dense zig-zag stitching on high-load spots, like cargo pocket corners, belt loops, and the base of a zipper fly. That reinforcement keeps the garment from tearing under extreme use.
Sewing being done does not mean the garment is finished. The final “Trim” phase dictates how the product will be perceived by the end consumer or the wholesale buyer.
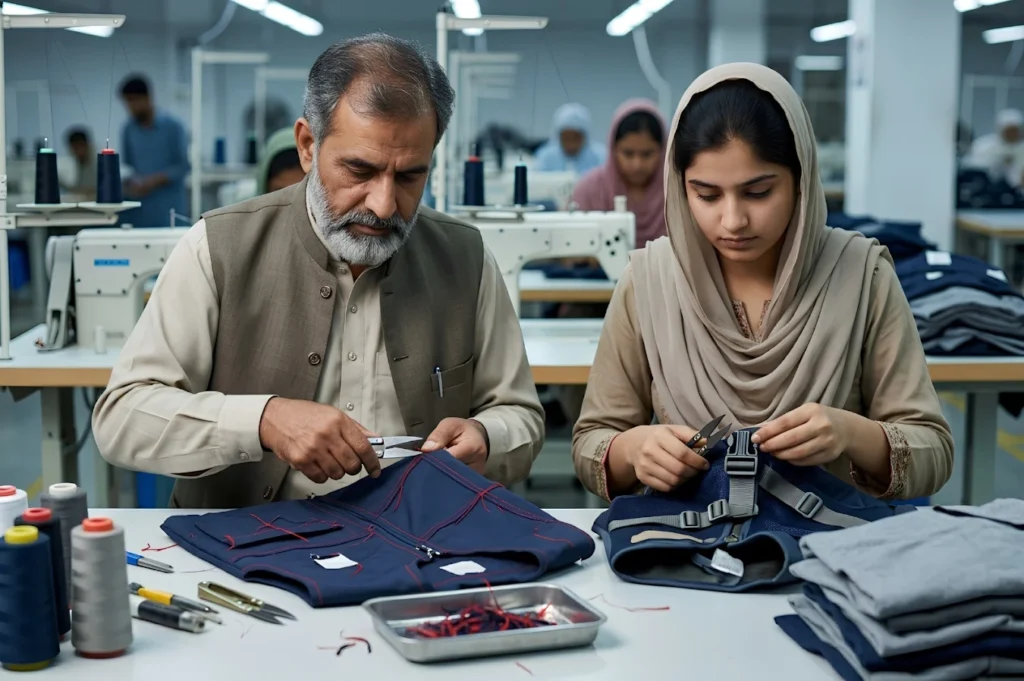
Fast industrial machines leave "thread tails" at the end of each seam. A trim crew checks each piece by hand, clipping stray threads and confirming every hardware fitting sits tight before packing.
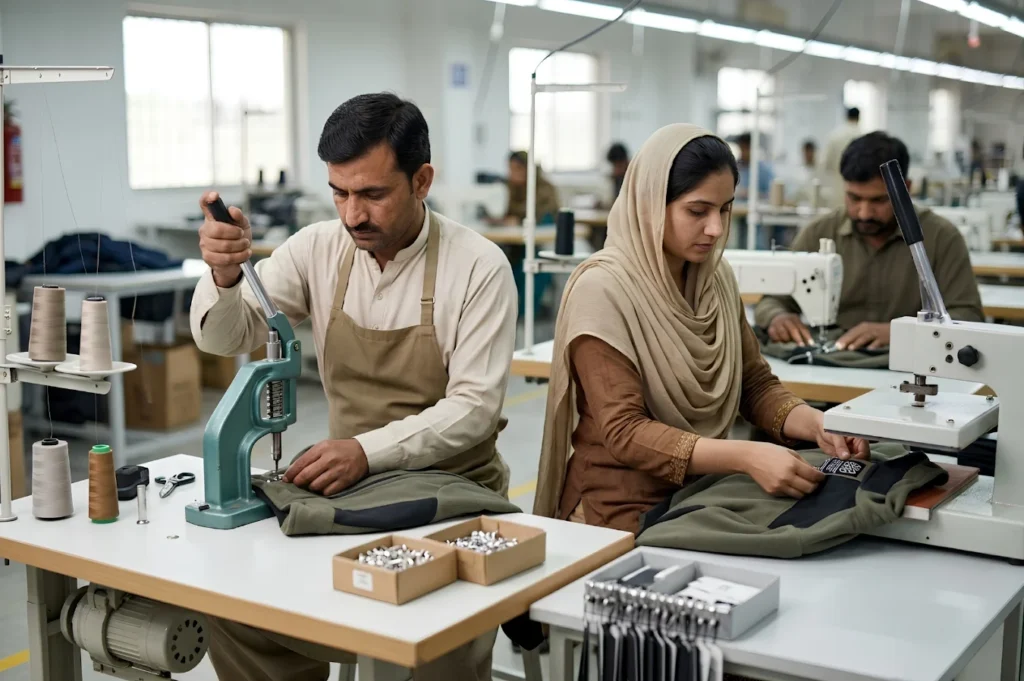
In a CMT model, you supply the trims. During this phase, our operators attach your custom woven neck labels, punch in metal rivets, install the supplied YKK zippers, and attach the final retail hang tags based precisely on the coordinates listed in your tech pack.
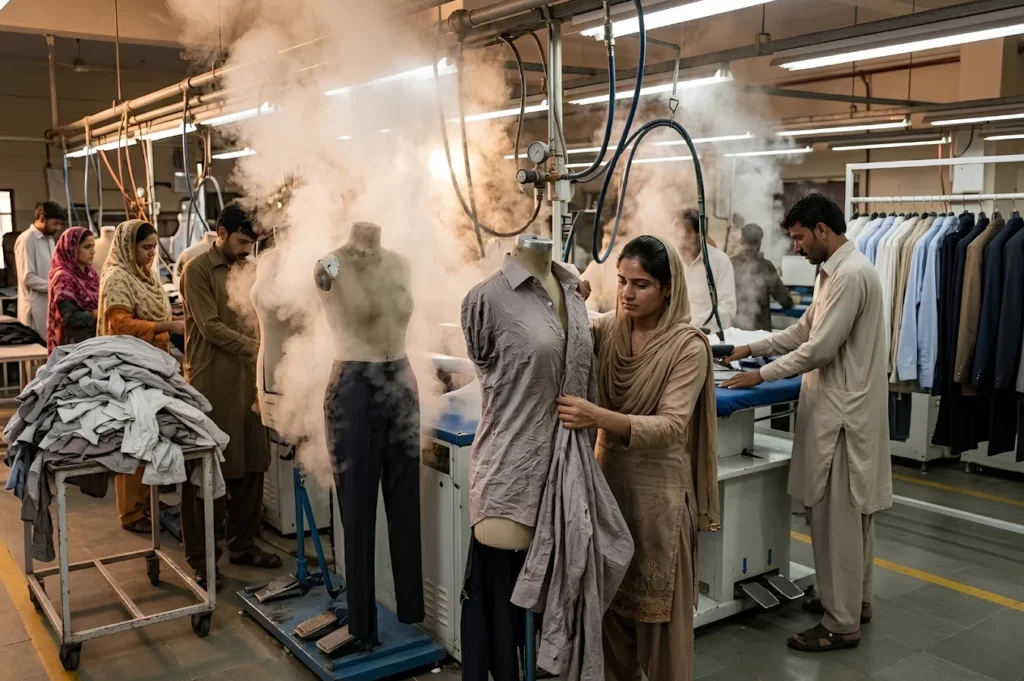
Cloth picks up wrinkles and distortion when it is handled heavily during sewing. Prior to packing, each piece is placed on pressing forms and hit with high-pressure steam. The steam flattens the seams, eases out small distortions in the cloth, and leaves a retail-ready drape on every piece.
Depending on the scale and structure of your supply chain, you must decide how much control you want to retain. Understanding the difference between these two models is critical before initiating a bulk run.
There is a major fear among brands using cut make trim clothing manufacturer services: Will the factory steal my excess fabric?
Transparency is our core operating principle. We do not operate in a black box. Before we cut a single yard of your supplied material, we run your graded patterns through advanced CAD nesting algorithms to generate a digital marker. This tells us the exact mathematical fabric yield required for the run.
Upon completion of the project, we provide a full Fabric Consumption Report. This document details exactly how many yards were received at our loading dock, how many yards were used to cut the garments, and how many yards remain as scrap or excess on the roll. If you request it, the excess fabric rolls are shipped back to you alongside the final garments.
Quick sewing is wasted money when defect rates run high, so speed alone is never the goal. A professional CMT factory does not wait until a 5,000-unit run is completely finished to start checking for errors. QC checks are built straight into the sewing line itself.
During the active sewing phase, our floor managers conduct random, continuous in-line audits. They pull garments directly off the sewing stations to measure Seams Per Inch (SPI) and inspect for thread tension issues. If a machine is dropping stitches or puckering the fabric, the entire line is halted. The machine is recalibrated immediately before the defect can replicate across the rest of the batch.
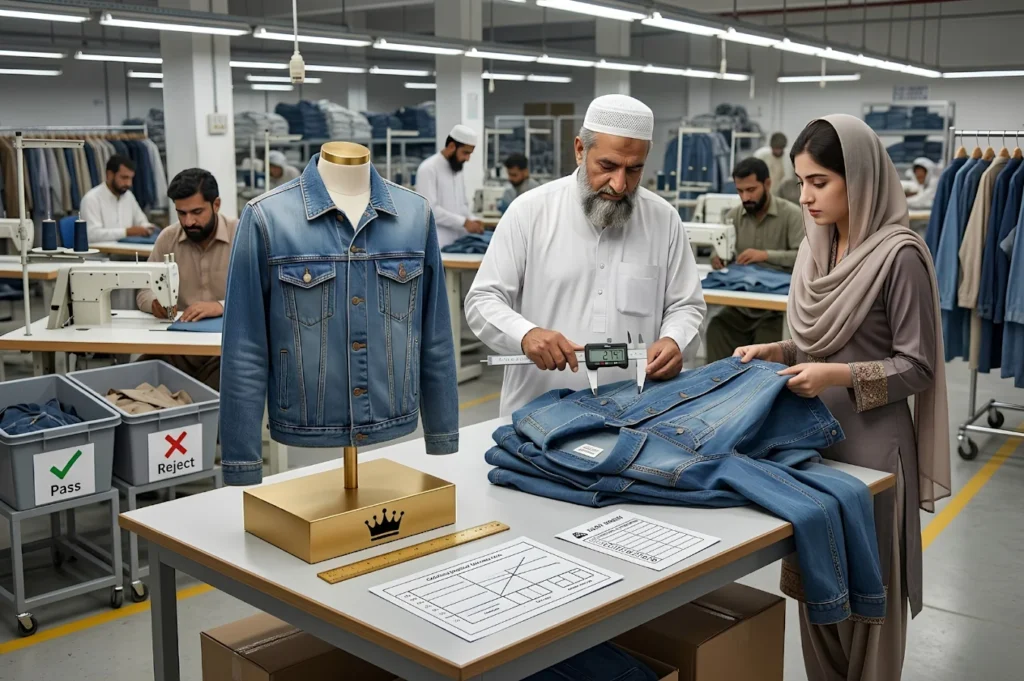
Quality is not subjective; it is contractual. Before bulk CMT production begins, you sign off on a physical Pre-Production (PP) sample. This physical garment is placed directly on the factory floor. Our QC inspectors measure the bulk garments against this "Golden Sample." If a collar width on the bulk run deviates from the Golden Sample beyond the allowed mathematical tolerance (e.g., +/- 0.25 inches), the unit is instantly rejected.
No plant should begin a bulk cut based on guesswork. For accuracy, we need these technical files locked, checked, and signed off before your cloth ever reaches the spreading tables.
We require finalized digital pattern files (DXF/ASTM). More importantly, those patterns must be nested into a high-yield "marker" file to ensure that when the CNC machine cuts your expensive fabric, waste is minimized to protect your margins.
The sewing operators must know exactly what components to pull from the bins. The Bill of Materials must explicitly list the exact zipper gauge, the specific placement coordinates for all woven labels, and the required thread weight.
All bulk fabrics, trims, buttons, and labels must arrive at our facility simultaneously. We cannot begin a CMT run if the fabric has arrived but the zippers are delayed in customs. If you are missing the digital assets, your project must first be routed through our [Pattern Making and Tech Pack Development Hub].
Sewing is just one link in a supply chain that has to work end to end, start to finish. To keep your run on track, read these related technical guides first:
Learn how we establish the Golden Sample before moving to the bulk cutting phase.
If you do not want to supply your own materials, understand how our FPP model sources and dyes raw greige goods.
Explore how visual branding is applied during the cut and sew process.
A heavyweight 100% cotton hoodie that measures perfect off the line but shrinks 5% in the buyer's washer is still a failed garment. We require strict wash testing at the prototype stage. We calculate the exact shrinkage percentage of your supplied fabric and artificially inflate the digital patterns by that exact percentage before the CNC machine cuts them. Straight off the machines the piece looks a little big, then it washes down to the intended size.
Before any cutting, your cloth goes through inspection machines to catch mill faults such as weave errors or dye spots. When serious faults turn up in your material, we stop the run and alert you at once so you can raise a claim with the mill.
Once the Golden Sample is approved, the tech pack is locked, and all of your physical raw materials have arrived on our factory floor, a standard CMT run typically takes 4 to 6 weeks. That window covers CNC cutting, line sewing, and strict AQL checks.
Yes. During the closing "Trim" stage, we can fold, tag, and poly-bag each piece to your exact retail specs. Barcode stickers and warning labels can also go on, so stock is ready for Amazon FBA or your 3PL warehouse.
Your costly cloth deserves better than a shop that takes shortcuts. One off-line blade or badly tuned sewing head can wreck thousands of dollars of custom-milled cloth.
Say goodbye to crooked seams, popped threads, and uneven sizing. Our floors bring the strict industrial discipline needed to run your tech pack cleanly at volume.
Rijix Limited - 7 Bell Yard, London, England, WC2A 2JR
Rijiz International - Mohala Chawinda Daburji Arayian Pasrur Road Sialkot, Pakistan.
Phone : +44 7307582940 Phone : +92 336 140 8321