In the apparel industry, a beautiful tech pack and expensive raw fabric mean nothing if the cutting and assembly phases are compromised. If a blade shifts by a millimeter during the cutting phase, or if a sewing operator applies too much tension to a 4-way stretch fabric, the entire production run is effectively ruined.
Cut and sew manufacturing is not simply “putting clothes together.” It is a strict mechanical science. It requires balancing fabric yield algorithms, stitch tension matrices, and rigorous quality control (AQL) at every workstation on the factory floor.
At Rijiz, we operate an industrial cut and sew factory built for brands that demand precision over speed. This document breaks down the mechanical realities, the production models, and the exact machinery protocols required to execute a high-volume production run flawlessly.
Amateur brands spend months obsessing over design but completely ignore the cutting process. In reality, the cutting room is where the profit margins of your entire collection are determined. Fabric is the single highest cost variable in garment production. How that fabric is laid out, tensioned, and sliced dictates your raw material waste.
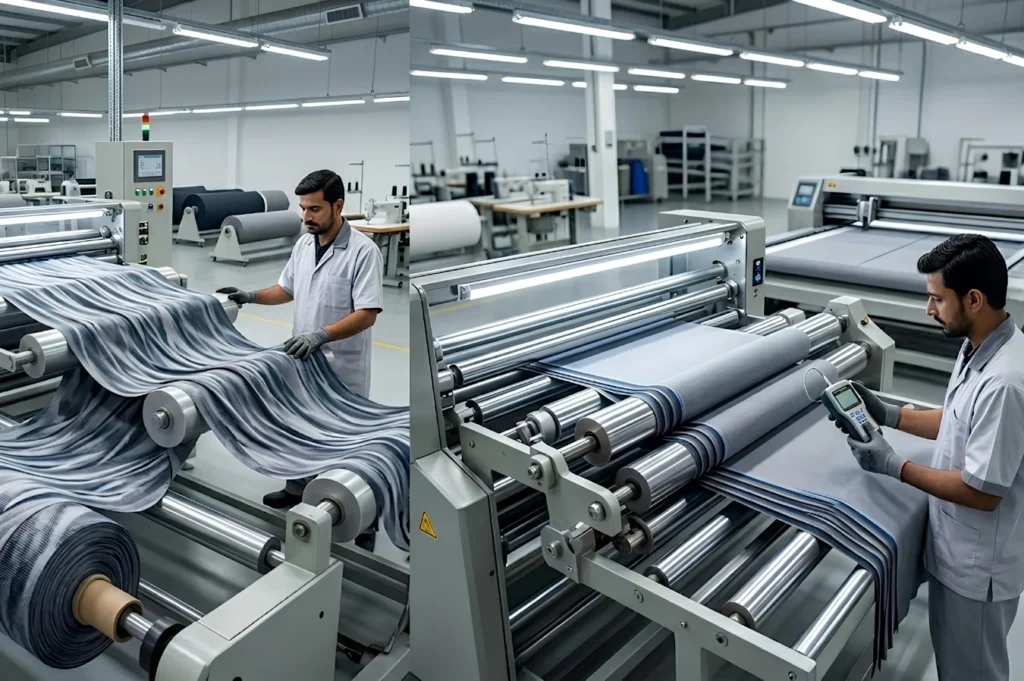
Before a single blade is engaged, massive rolls of fabric are unspooled and layered onto cutting tables in stacks known as "plies." If the fabric is pulled tightly during this spreading process, it retains kinetic tension. Once the fabric is cut, that tension releases, and the cut panels instantly shrink. If a facility does not employ automated, zero-tension spreaders, your final garments will be mathematically smaller than your approved pattern.
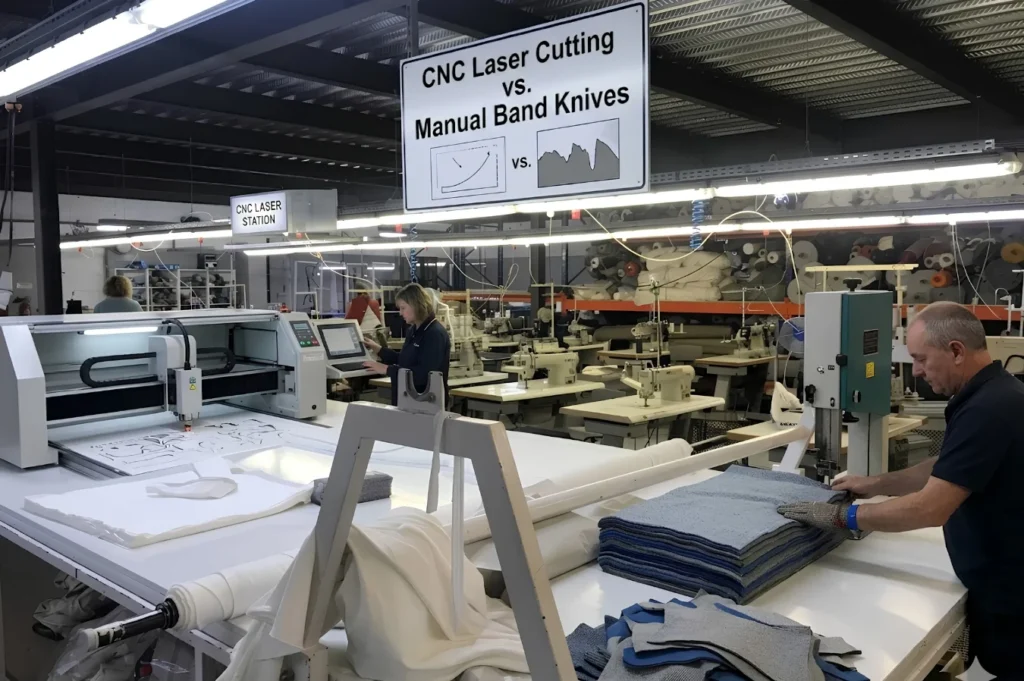
Manual tracing and cutting with hand shears are acceptable for a single prototype, but they are catastrophic for bulk runs. We deploy automated CNC (Computer Numerical Control) cutting machines. Your digital DXF marker files are fed directly into the machine, which cuts through heavy 450 GSM fleece or delicate activewear with micro-millimeter precision. For extreme-density fabrics, our operators utilize industrial band knives to prevent fraying and edge distortion.
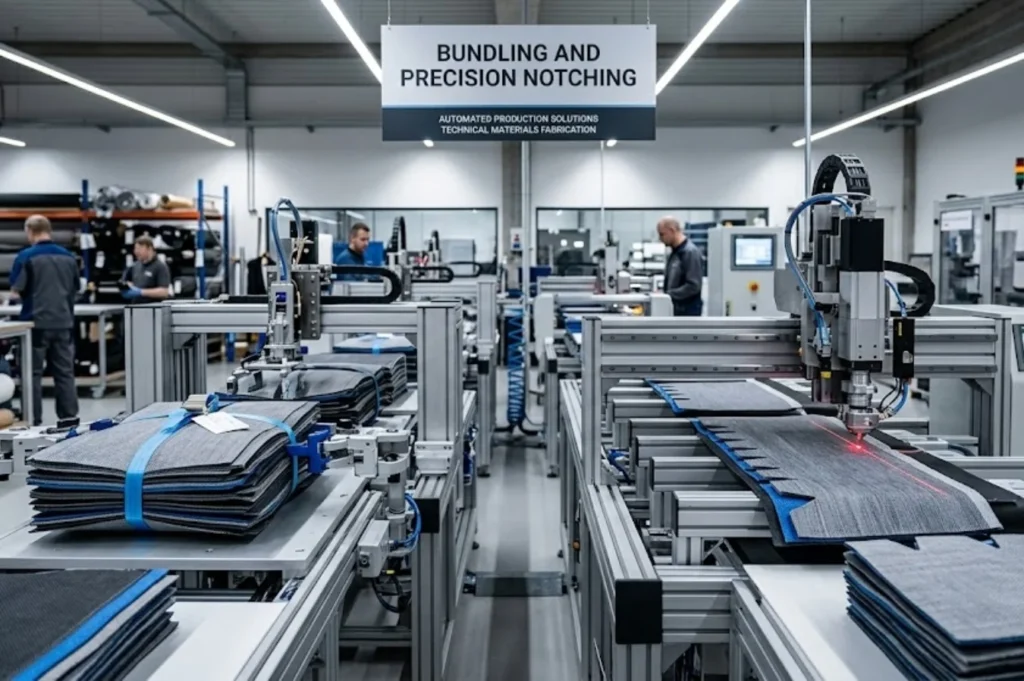
Once the fabric is cut, every piece is bundled and labeled before it hits the sewing floor. During the cutting phase, the CNC machine punches exact drill holes and V-notches into the perimeter of the fabric. These industrial markers tell the sewing operators exactly where to align a pocket, a sleeve cap, or a dart, completely removing guesswork from the assembly line.
Depending on the scale and structure of your supply chain, we offer two distinct avenues for bulk assembly. Understanding which production model fits your current operational capacity is crucial before initiating a run with any cut and sew apparel manufacturer.
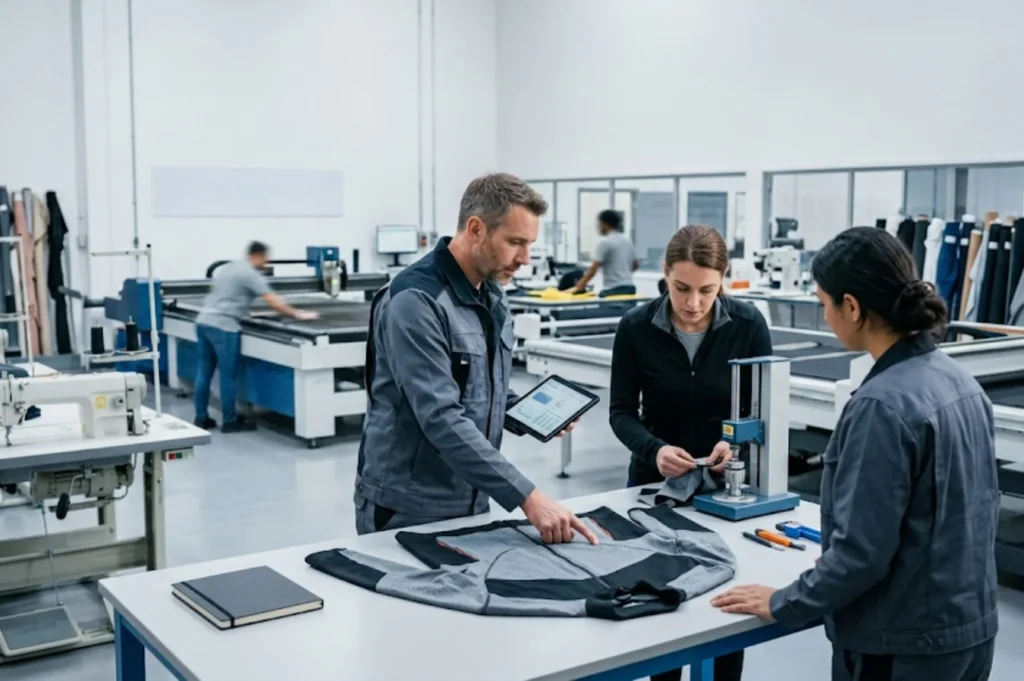
In a CMT manufacturing model, the brand acts as the primary supplier. You purchase the raw fabric, source the custom zippers, buy the woven labels, and ship all the physical raw materials directly to our loading dock. We provide the labor and the machinery: we Cut the fabric based on your marker, Make (sew) the garment, and Trim (finish and package) the final product.
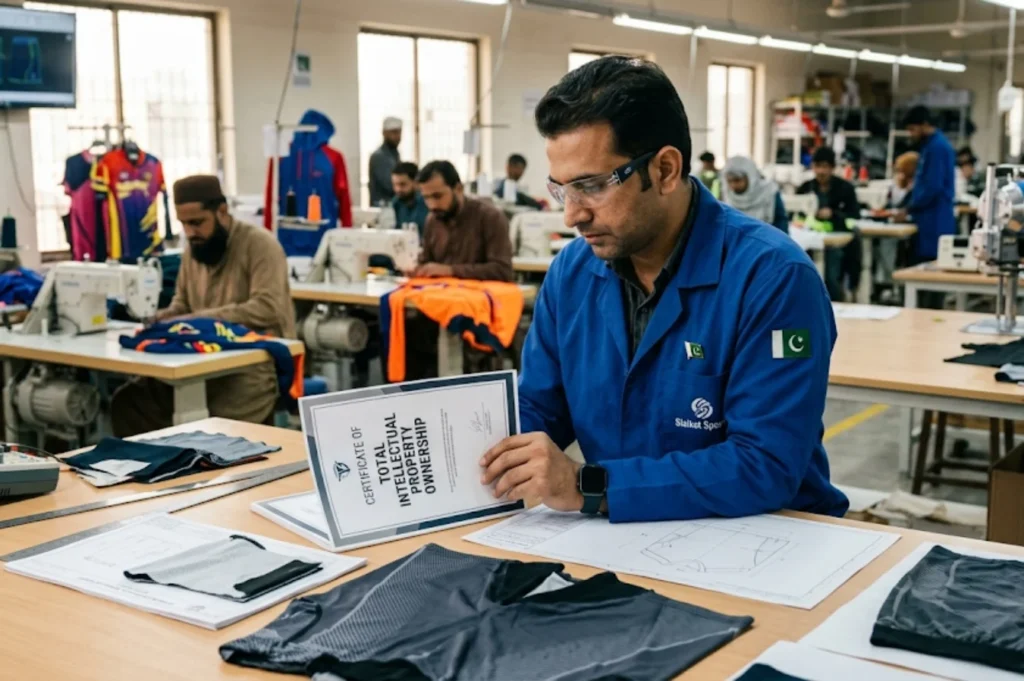
For brands that want a single point of accountability, the Full Production Package (often referred to as OEM) is the industry standard. In this model, you provide the technical blueprint (the Tech Pack), and we handle the entire supply chain. We source the raw greige fabric, manage the Dye-to-Match (DTM) lab dips, engineer the patterns, and execute the final custom cut and sew services. FPP eliminates the logistical nightmare of coordinating between a fabric mill, a dye house, and a sewing floor.
A standard straight-stitch sewing machine cannot build a complex technical garment. Different fabrics and structural stress points require entirely different mechanical setups. A premium contract sewing services facility must maintain a diverse fleet of specialized machinery to prevent seam failure.
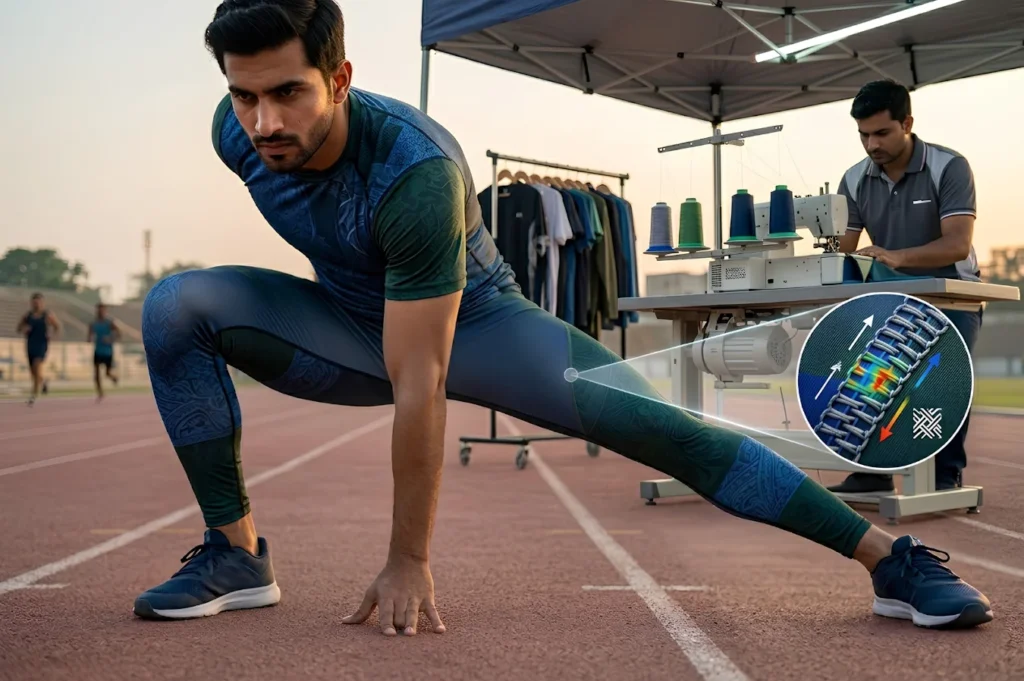
If you sew four-way stretch spandex with a standard rigid lockstitch, the thread will snap the moment the end-user puts the garment on. For activewear, swimwear, and performance gear, we deploy 4-thread overlock and coverstitch machines. These machines loop the thread in a way that allows the seam to stretch simultaneously with the fabric. Furthermore, we utilize flatlock stitching to eliminate interior seam chafing on tight-fitting athletic wear.
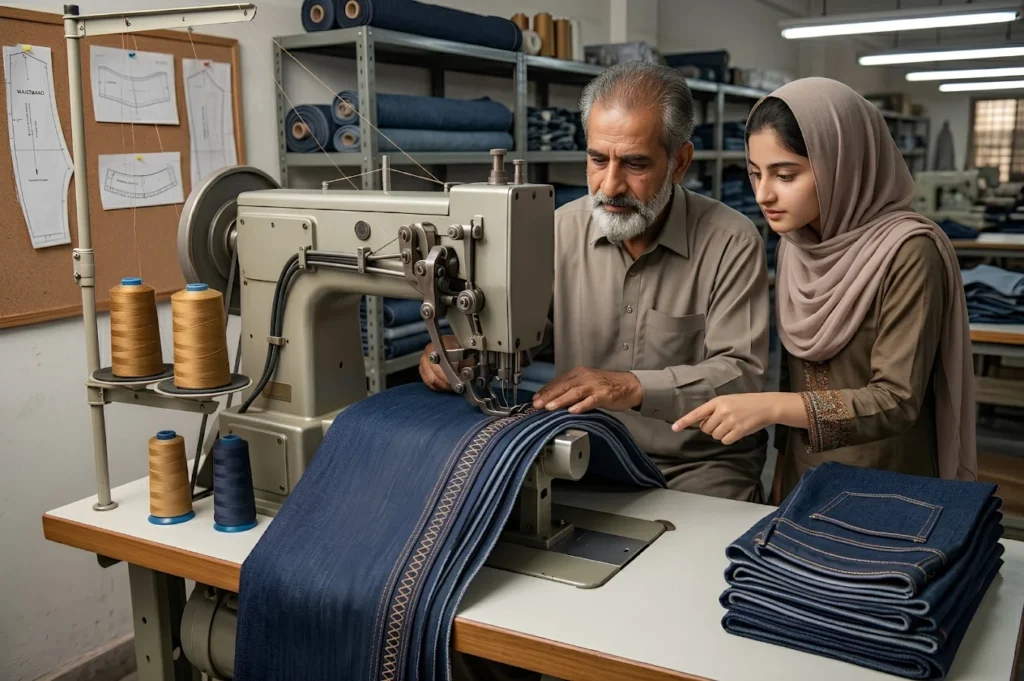
Working with 14oz raw denim or 400+ GSM French Terry requires immense mechanical torque. Standard sewing machines will skip stitches or snap needles when attempting to penetrate multiple layers of heavy fabric. We utilize heavy-duty walking-foot machines that feed the thick layers of fabric evenly through the needle plate, ensuring the top layer does not bunch up or shift out of alignment.
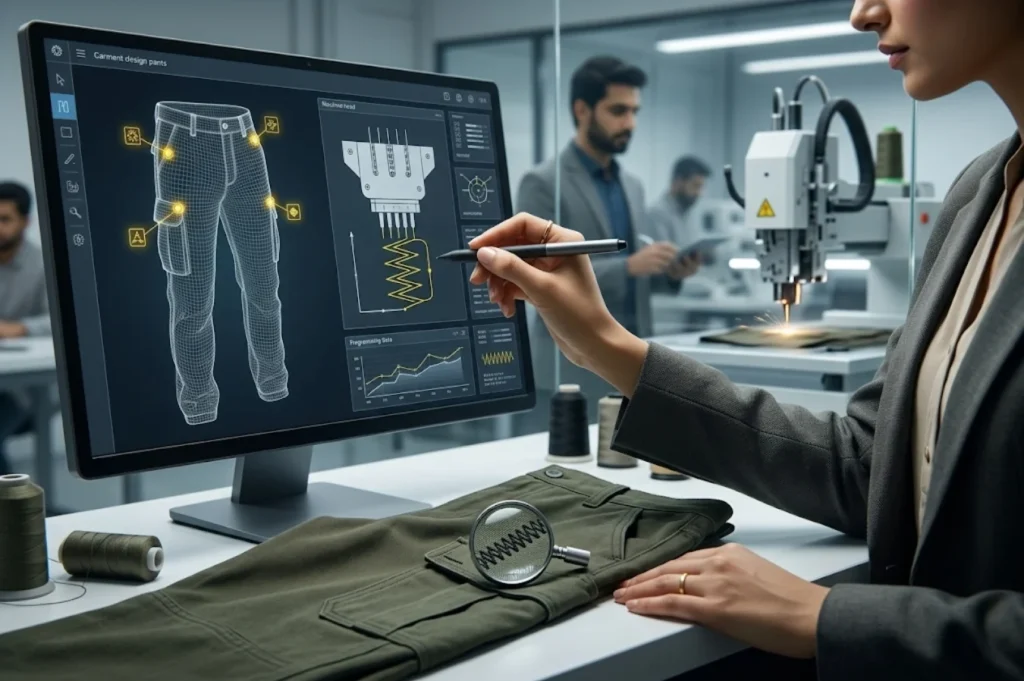
Workwear and premium streetwear must endure heavy physical strain. We program automated bar-tack machines to fire concentrated zig-zag stitches over the specific stress points of the garment—such as the corners of cargo pockets, belt loops, and the base of a zipper fly. This industrial reinforcement ensures the garment does not tear during extreme use.
The raw edge of a cut piece of fabric will naturally fray and unravel. How that edge is treated inside the garment is the defining difference between cheap fast fashion and luxury apparel.
Fast sewing is financially useless if it results in high defect rates. A professional factory does not wait until a 5,000-unit run is completely finished to start checking for errors. Quality Control must be built directly into the assembly line workflow.
A garment is not finished just because the sewing is complete. The final presentation of the product dictates how it will be perceived by the end consumer or the wholesale buyer.
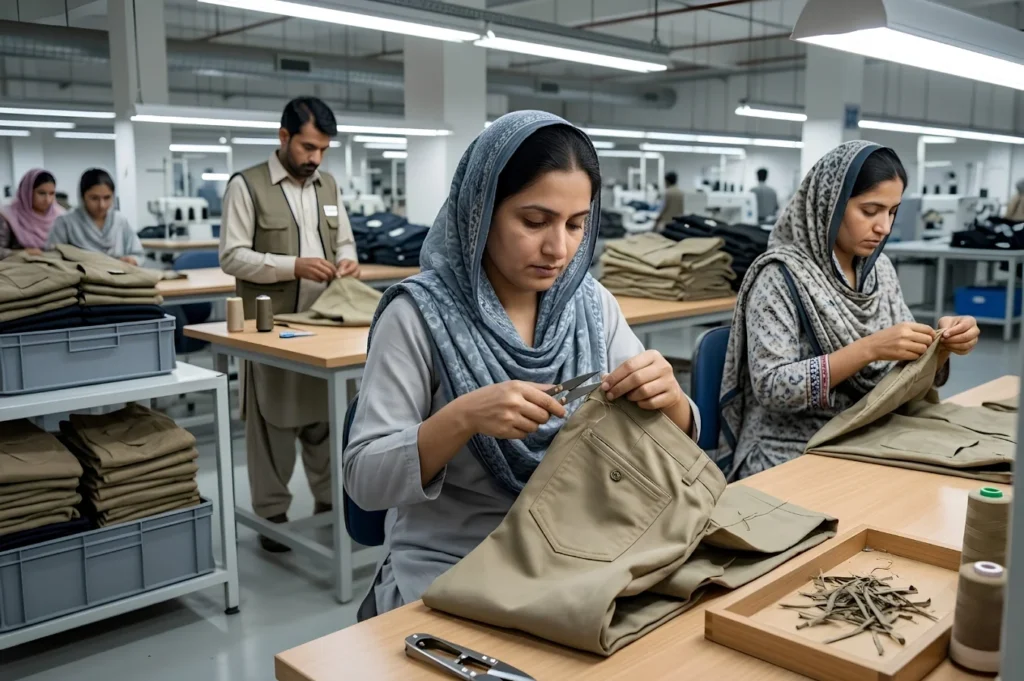
High-speed industrial sewing leaves "thread tails" at the end of every seam. Dedicated trimming operators manually inspect every inch of the garment, snipping away loose threads and verifying that all bar-tacks are securely locked in place.
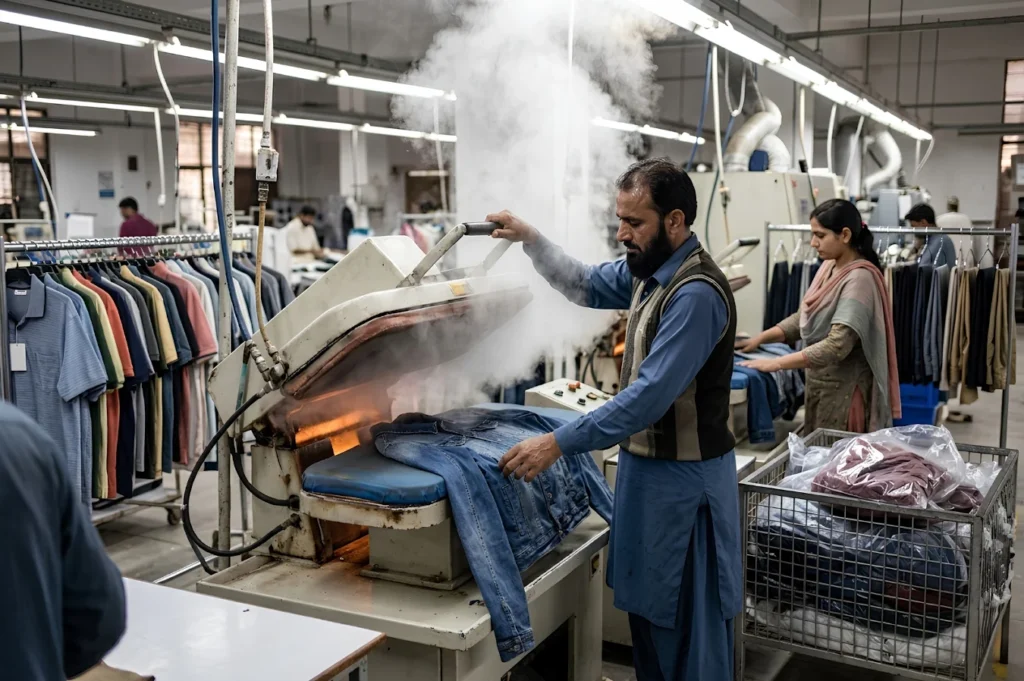
Fabric becomes wrinkled and distorted during the heavy handling of the sewing process. Before packaging, every garment is mounted on industrial ironing bucks and treated with high-pressure steam. This process forces the seams to lay completely flat, shrinks any minor fabric distortions back into place, and gives the garment its final, retail-ready drape.
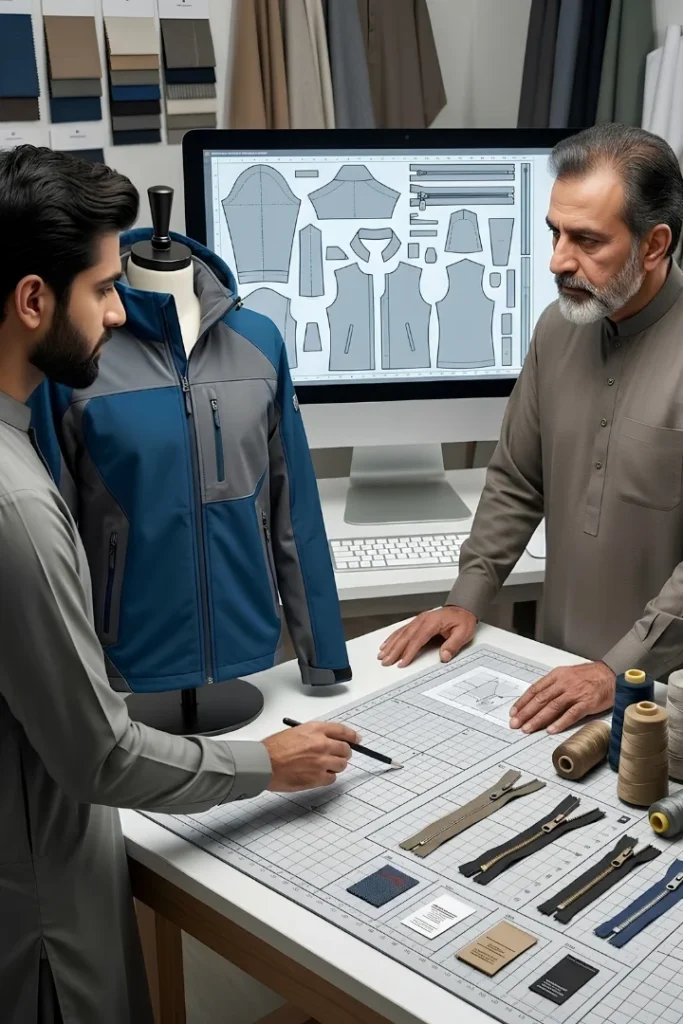
A factory cannot start a bulk cutting run on an assumption. To ensure precision, we require the following technical assets to be locked, verified, and approved before the fabric is ever loaded onto the spreading tables.
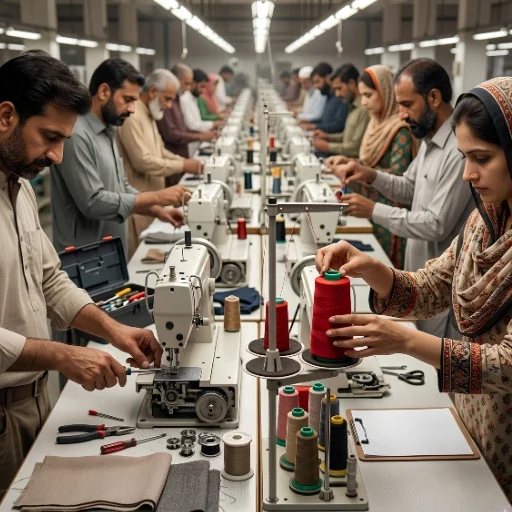
Setting up a factory line is highly labor-intensive. It requires calibrating the CNC lasers, changing the thread cones on 30 different sewing machines, and adjusting the feed-dogs for your specific fabric weight.
Because of this intense setup time, true industrial facilities enforce Minimum Order Quantities (MOQs). Running micro-batches is economically unviable, as the setup costs would drastically inflate the price per unit, making it impossible for your brand to maintain a profitable retail markup.
The assembly line is only one component of a successful supply chain. To ensure your production run is executed perfectly, we recommend reviewing our related technical guides:
Learn how we establish the Golden Sample before moving to the bulk cutting phase.
Explore how visual branding is applied during the cut and sew process.
Understand the FPP model and how we source, knit, and dye raw greige goods.


 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.

 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.
 Trustindex verifies that the original source of the review is Google.
Transparency is our core operating principle. During a CMT run, we calculate the exact fabric yield based on the digital marker. We provide a full consumption report detailing exactly how many yards were used to cut the garments and how many yards remain as scrap.
If a heavyweight 100% cotton hoodie is sewn perfectly to size but shrinks by 5% in the customer's washing machine, the product is a failure. We mandate strict wash-testing during prototyping. We calculate the exact shrinkage percentage of the raw fabric and artificially inflate the digital patterns by that exact percentage before the CNC machine cuts them. The garment will look slightly oversized coming off the sewing line but will shrink to the perfect dimensions after its first wash.
Once the Golden Sample is approved and the bulk fabric is secured on the factory floor, a standard cut and sew run typically takes 4 to 6 weeks. This timeline accounts for the CNC cutting, the assembly line sewing, and the rigorous AQL inspection phases.
Yes. As part of our final trimming and finishing phase, we can fold, tag, and poly-bag every garment to your exact retail specifications. We can apply custom barcode stickers and warning labels so the inventory is instantly ready for Amazon FBA or your 3PL warehouse.
Do not trust your raw materials to a facility that cuts corners. A single misaligned blade or a poorly tensioned sewing machine can ruin thousands of dollars of custom-dyed fabric.
Stop dealing with crooked seams, popped threads, and inconsistent sizing. Our production floors provide the hard industrial discipline needed to execute your tech pack flawlessly at scale.
Fast & secure delivery worldwide.
Hassle-free refunds
Confidence in every purchase.
Dedicated customer assistance.
Rijix Limited - 7 Bell Yard, London, England, WC2A 2JR
Rijiz International - Mohala Chawinda Daburji Arayian Pasrur Road Sialkot, Pakistan.
Phone : +44 7307582940 Phone : +92 336 140 8321